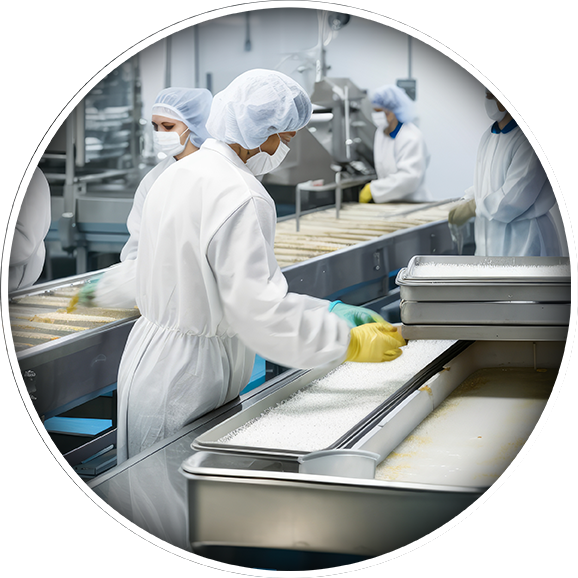
FACILITY & CAPABILITIES
Built for consistency, speed, and food safety, our Surrey, BC facility integrates cooking, packaging, freezing, and cold-chain logistics under one roof.
Production Capacity
- 5 tons / day of prepared meals
- State-of-the-art operation running 5 days / week
Certifications
- USDA, CFIA, HACCP, SQF Level 2, HALAL
Capabilites
- End-to-end cold chain management
- Sous-vide boilable pouches (BPA-Free)
- Modified Atmosphere Packaging (MAP)
- High-Pressure Processing (HPP)
- Biodegradable Trays
This fully integrated environment enables us to maintain quality, accelerated throughput, and support both chilled and frozen programs with confidence.